CIP vs SIP: What’s the Difference for Hygienic/Sanitary Equipment
CIP (clean-in-place) removes product residue from equipment without disassembly, using water, detergent, and acid rinses. SIP (steam-in-place) follows CIP and inactivates microorganisms with saturated steam at 121 °C (250 °F) or higher. Nearly every sanitary process uses CIP. Only sterile and aseptic processes need SIP, and that requirement changes which valves, gaskets, and instruments you can use.
Spec sheets use “CIP” and “SIP” as if they described the same thing at different strengths. A requirement reads “CIP/SIP capable” and gets copied from one project to the next without anyone asking which process needs which. The result lands in one of two places. A line that only needs CIP ends up with steam-rated components it never uses, and the budget absorbs the difference. A line that needs SIP ends up with gaskets, instruments, or piping that cannot take steam, and the gap shows up at commissioning or audit.
That habit is the villain of this guide. CIP and SIP solve different problems, they are validated differently, and they place different demands on every component in the system. Deciding which one a process needs comes first, and component selection follows from that decision.
This article covers what each process does, how a cycle runs, how to decide between CIP alone and CIP plus SIP, and how the answer reaches valves, gaskets, pumps, instruments, and piping. It spans the whole sanitary system by design, so it applies to pump lines and valve manifolds alike.
TL;DR
- CIP removes soil and residue, and SIP inactivates microorganisms. SIP follows CIP on the same equipment.
- Four factors set CIP effectiveness: time, temperature, chemical concentration, and mechanical action.
- SIP depends on holding saturated steam at 121 °C (250 °F) or higher at the coldest point in the system, with condensate drained from every low point.
- Product risk and the governing standard decide whether a process needs SIP. Most food and beverage lines run CIP with a sanitizing step, and sterile pharmaceutical and biotech lines add SIP.
- The choice reaches valve type, gasket compound, pump seals, instruments, and piping slope.
- A six-step specification process turns the decision into written requirements and a verification plan.
What this article covers
- What do CIP and SIP stand for, and what does each one do?
- How do CIP and SIP compare side by side?
- How does a CIP cycle work?
- How does a SIP cycle work?
- When does a process need SIP, and when is CIP alone enough?
- How does the CIP or SIP decision change valve selection?
- How does it change gasket and elastomer selection?
- How does it change pump and seal selection?
- How does it change instrumentation and piping design?
- What are the most common CIP and SIP specification mistakes?
- How do you specify the cleaning approach for a system in six steps?
What do CIP and SIP stand for, and what does each one do?
CIP stands for clean-in-place and SIP stands for steam-in-place. CIP removes product residue and soil from equipment surfaces, and SIP sterilizes those surfaces with steam. Both run without taking the equipment apart.
Defined Term: CIP (clean-in-place)
an automated cleaning process that circulates water, detergent, and acid solutions through process equipment and piping without disassembly, removing product residue to a validated limit.
Defined Term: SIP (steam-in-place)
an automated sterilization process that holds saturated steam in process equipment and piping, without disassembly, long enough at a validated temperature to inactivate viable microorganisms. Some sources spell SIP out as sterilize-in-place.
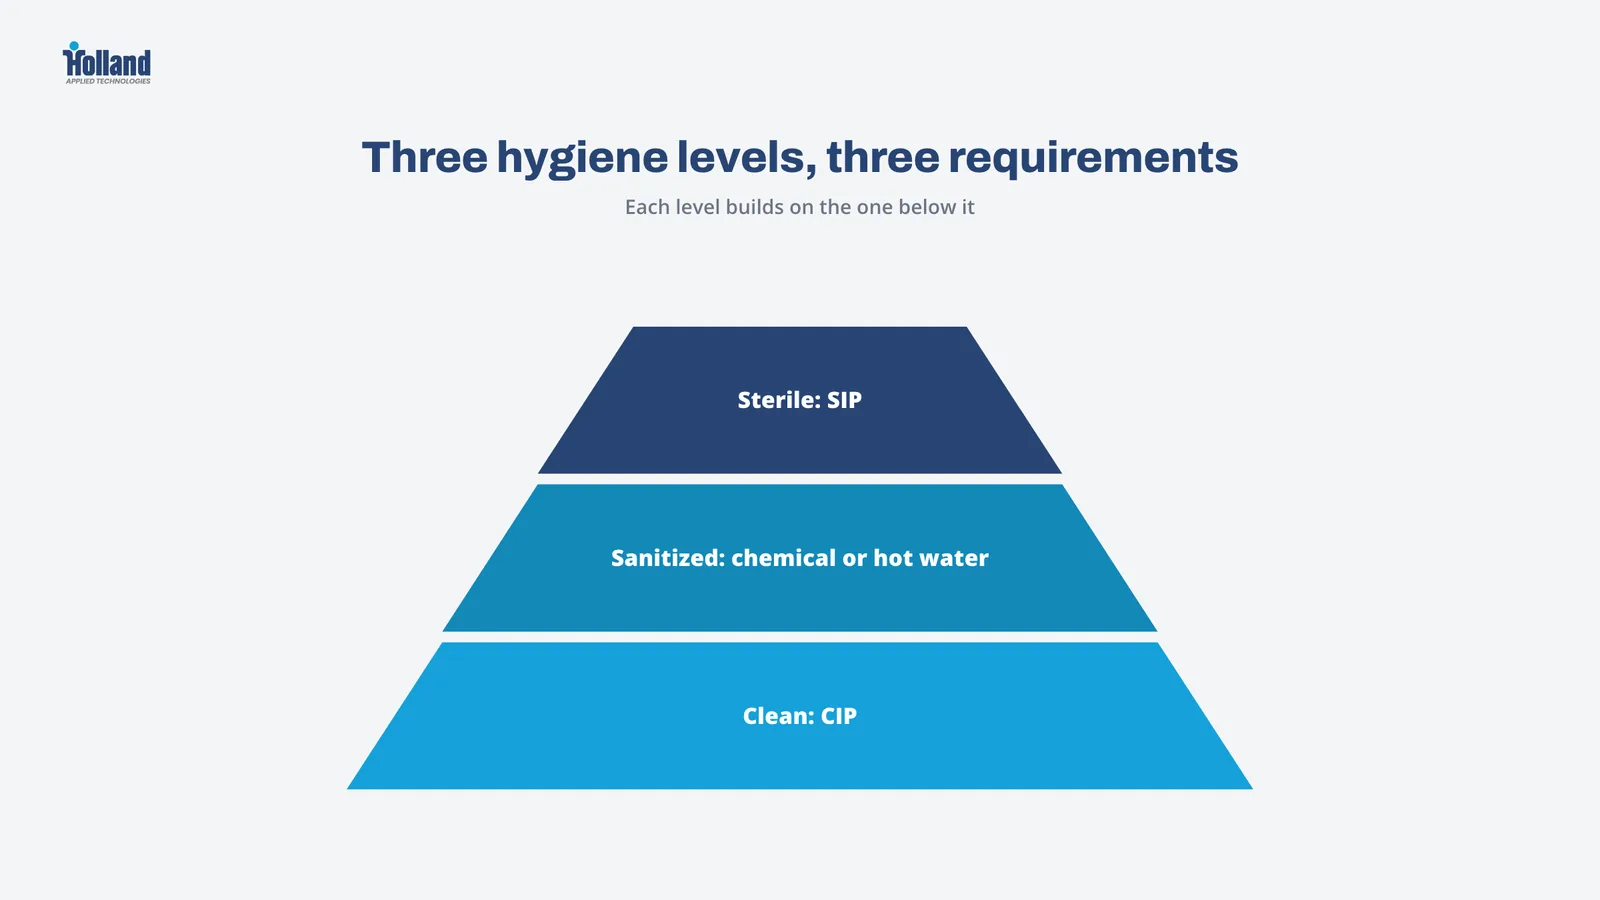
Read CIP as soil removal
CIP targets the product film on the surface: proteins, fats, sugars, minerals, and biofilm precursors. The goal is a surface that meets a residue and microbial limit set during validation. CIP leaves the system clean to a validated limit, and sterility takes a separate step.
Read SIP as microbial inactivation
SIP targets living microorganisms. The goal is a defined sterility assurance level, commonly written as 10⁻⁶, which sets the acceptable probability of a surviving organism. SIP depends on a clean surface. Residue left on a surface can shield organisms from the steam, so CIP always runs first.
Place sanitizing between the two
A third level sits between clean and sterile. Sanitizing reduces microbial counts with a chemical sanitizer or hot water, usually as the final step of a CIP cycle. Many food and beverage lines stop at this level. Sterile processes continue to SIP.
A companion post on what CIP stands for covers the acronym and the basic concept for readers who are new to it. This guide assumes you know the terms and need to decide how to apply them.
How do CIP and SIP compare side by side?
CIP removes soil and runs first, and SIP inactivates microorganisms and runs second. CIP uses liquid chemistry and mechanical action, and SIP uses saturated steam at 121 °C (250 °F) or higher. CIP is nearly universal, and SIP is specific to sterile and aseptic processes.
| Variable | CIP (clean-in-place) | SIP (steam-in-place) |
|---|---|---|
| Purpose | Remove product residue and soil | Inactivate viable microorganisms |
| Medium | Water, detergent, acid, and rinses | Saturated steam |
| Typical temperature | Warm to hot wash, set by the chemistry and the soil | 121 °C (250 °F) or higher at the coldest point |
| Order in the sequence | First | After CIP |
| Validated outcome | Residue and microbial limits met | Sterility assurance level met |
| Needed by | Nearly every sanitary process | Sterile and aseptic processes |
| Main equipment demand | Drainable, cleanable geometry and chemically compatible materials | Steam-rated materials, condensate drainage, and temperature monitoring |
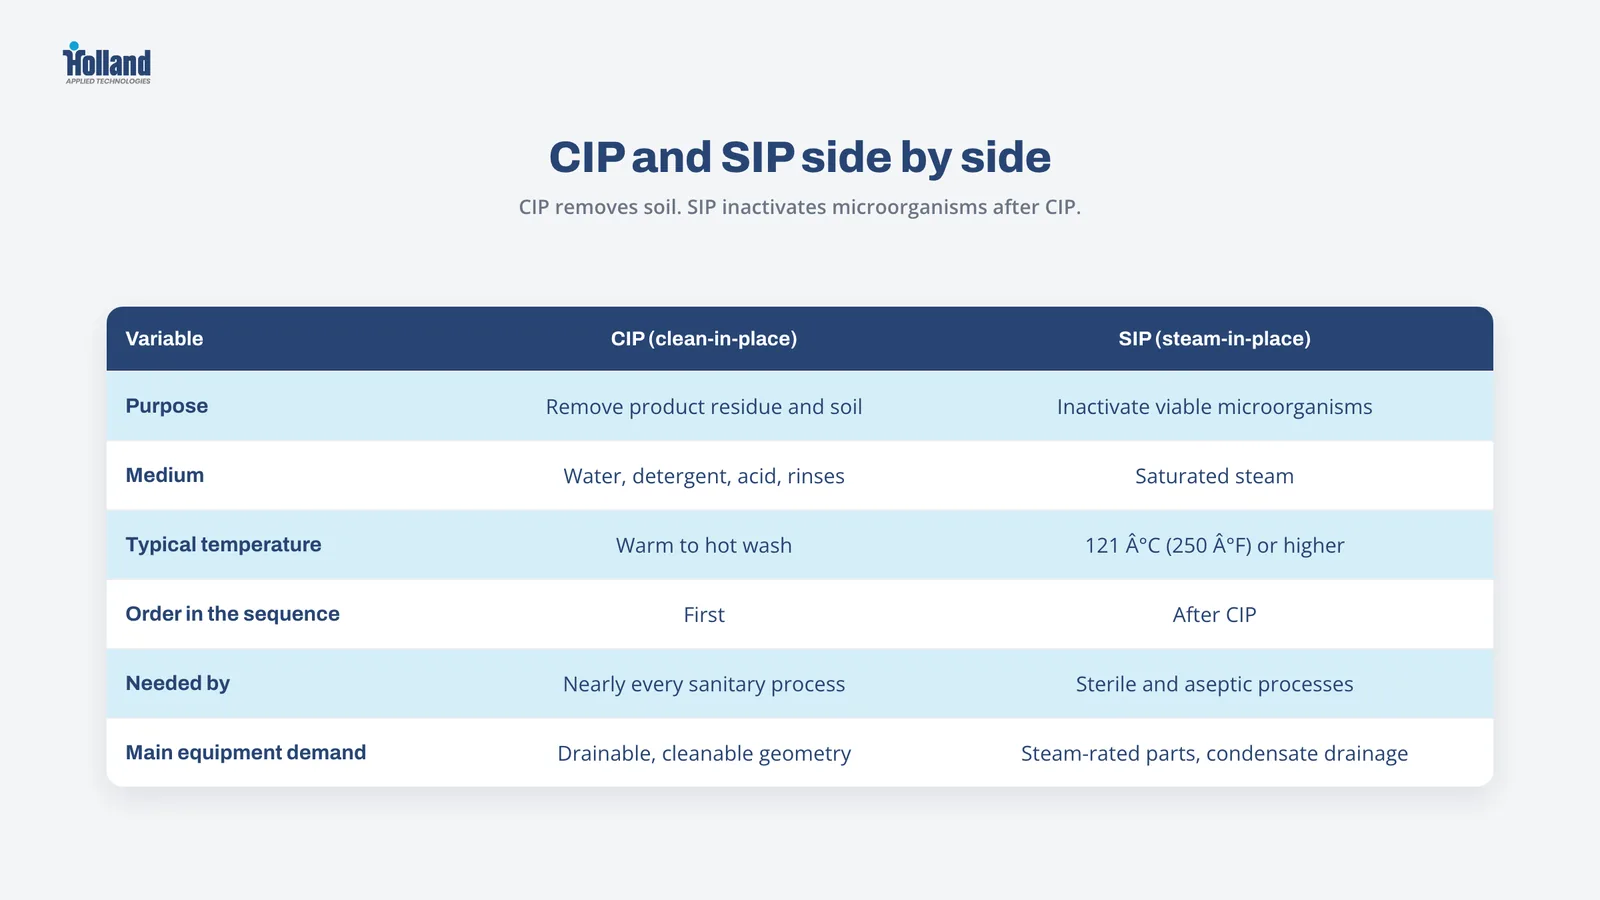
Read the last row first when you are specifying equipment. CIP asks the equipment to be cleanable and chemically compatible. SIP asks for everything CIP asks for, plus resistance to heat and a design that drains condensate. That added demand is where cost and risk concentrate.
How does a CIP cycle work?
A CIP cycle moves through a pre-rinse, a caustic wash, an intermediate rinse, an acid wash where needed, a final rinse, and often a sanitizing step. Four factors, time, temperature, chemical concentration, and mechanical action, set how well each step removes soil.
A typical sequence:
- Pre-rinse: water flushes bulk product out of the system and carries away loose soil.
- Caustic wash: a hot alkaline solution dissolves fats and proteins.
- Intermediate rinse: water removes the caustic before the next chemistry.
- Acid wash (as needed): an acid solution removes mineral scale and film that caustic leaves behind.
- Final rinse: water removes the last chemistry from the system.
- Sanitize (optional): a chemical sanitizer or hot water reduces microbial counts before production.
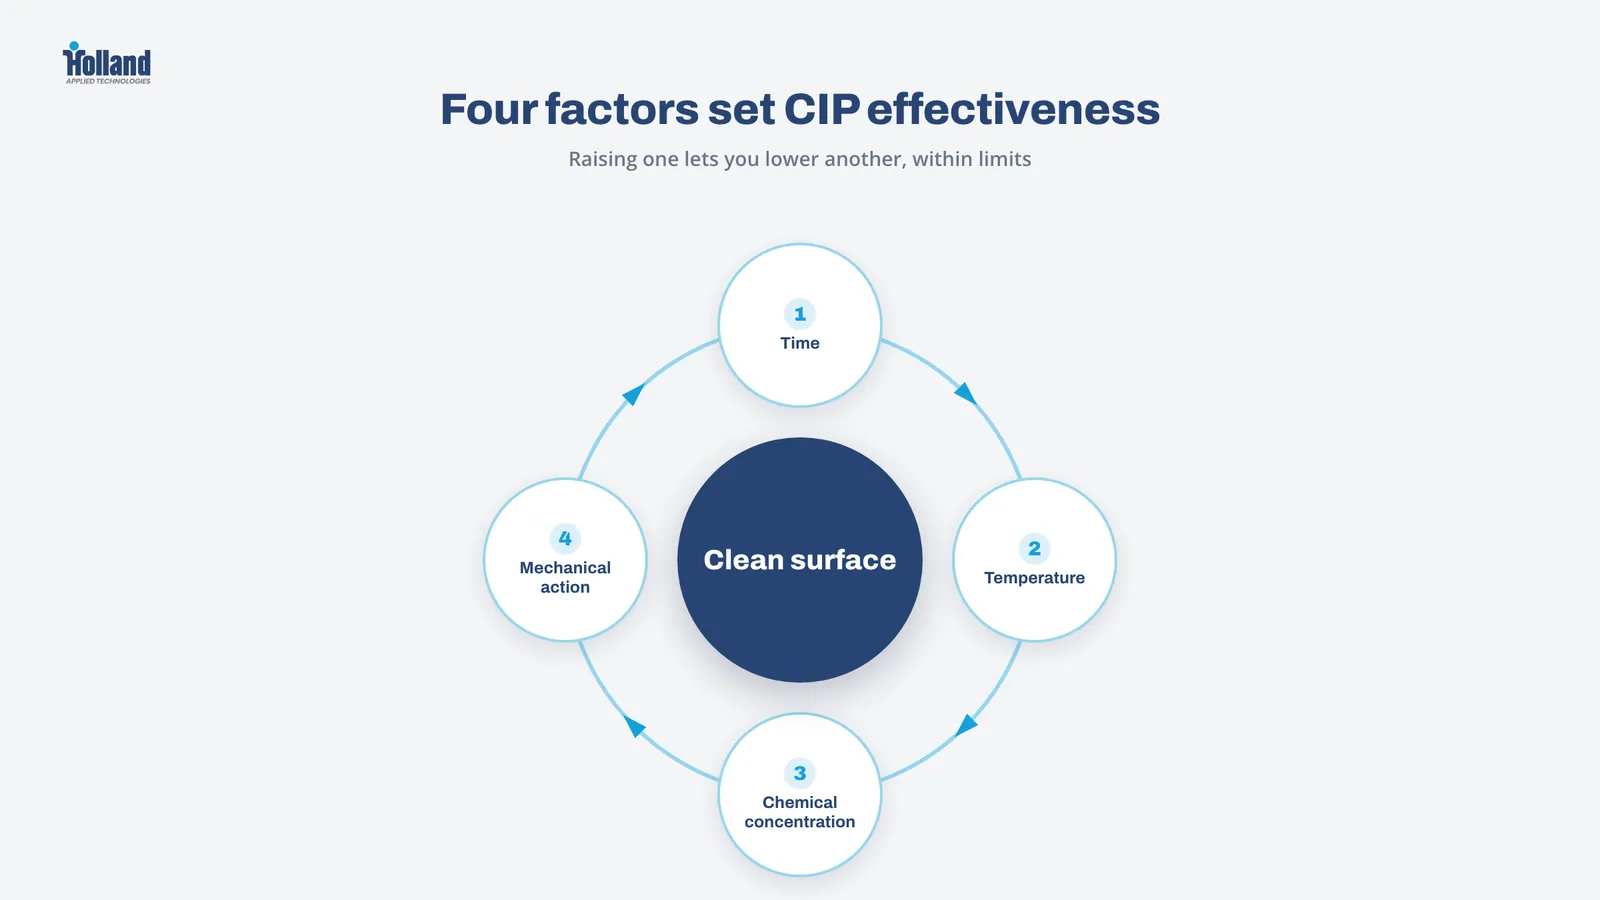
The four factors work together with no fixed order, and the numbers in the diagram label them without ranking them.
Set the flow velocity for turbulent flow in piping
Mechanical action in piping comes from flow velocity. A commonly cited target is about 5 feet per second (1.5 meters per second) in the pipe, which produces turbulent flow that scrubs the wall. Check the pump and the line size against that target during design. A pump that cannot reach it leaves the wall under-cleaned regardless of chemistry.
Verify that every surface the solution must reach is wetted
Chemistry only cleans what it touches. Vessels need spray devices that cover every surface, and branch lines need flow through or around them. Walk the piping drawing and mark each branch, dead end, and valve cavity, then confirm how the solution reaches each one. Holland’s earlier post on cleaning cycle time and valve choice shows how valve design affects that coverage and the hours behind it.
Record the cycle parameters on every run
Record time, temperature, concentration, and flow at each step. These records are the evidence that a cycle ran to its validated parameters, and they are the first thing an auditor asks for. Many plants log them automatically, and the specification should say so.
Ready to solve this?
Send over your piping layout, product, and cleaning chemistry, and Holland’s engineers will help you match components to your CIP cycle.
How does a SIP cycle work?
A SIP cycle starts from a clean, drained system, introduces saturated steam while venting air, brings the coldest point to temperature, holds for the validated time, and cools under positive pressure. The cycle is only as good as its coldest point.
A typical sequence:
- Complete CIP first: the surfaces have to be clean for steam to reach them.
- Drain the system: standing liquid cools steam and creates cold spots.
- Introduce steam and vent air: air trapped in the system blocks steam contact, so vents and drains open until steam fills the system.
- Bring the coldest point to temperature: steam reaches 121 °C (250 °F) or higher at the location that heats last.
- Hold for the validated time: the hold starts when the coldest point reaches temperature, and the time comes from validation.
- Cool under positive pressure: sterile air or gas replaces the steam as it condenses, so the system never draws in non-sterile air.
Defined Term: Coldest point
the location in a sterilized system that reaches temperature last, usually a low point or a spot far from the steam source where condensate collects. Validation places temperature probes there, and the hold time starts when that location reaches the target.
Locate the coldest point during design
Find the coldest point on the piping drawing before the system is built. Look at low points, dead ends, the far end of long runs, and places where condensate collects. Place a temperature sensor and a steam trap or drain at each one. A coldest point found at commissioning costs far more to fix than one found on the drawing.
Drain condensate at every low point
Steam condenses as it heats the metal, and the condensate has to leave. Slope piping toward drains and add steam traps or drain valves at each low point. Trapped condensate cools the surface and shields organisms from steam.
Cool under positive pressure with a sterile vent
When steam condenses, it leaves a vacuum behind. A system that cools without a gas supply can pull in non-sterile air through any opening. Specify a sterile gas supply or a sterile vent filter, and heat the filter housing so condensate does not wet the membrane. Holland’s post on the heated hydrophobic sterile tank vent explains why.
SIP is one of several sterilization methods. Holland’s post on autoclave, gamma, and ETO sterilization covers the others and where each fits.
When does a process need SIP, and when is CIP alone enough?
A process needs SIP when the product, the regulatory standard, or the validation plan requires a sterile product path. CIP with a sanitizing step is enough when the product is not sterile and the standard calls for a hygienic, cleanable system.
| Process | Typical approach | Reason |
|---|---|---|
| Dairy, beverage, and most food processing | CIP with a sanitizing step | The product path has to be hygienic and cleanable, and the product is not sterile |
| Biologics, parenteral products, and water-for-injection systems | CIP followed by SIP | The product path has to be sterile to protect the patient |
| Aseptic food lines | CIP followed by sterilization of the downstream path with steam or hot water | The product is sterile and the path after the sterilizer has to stay sterile |
| Non-sterile pharmaceutical manufacturing | CIP with a sanitizing step, with SIP where the process or the product calls for it | Cleaning validation sets the limit, and sterility depends on the product |
The table is a starting point. The final decision belongs to the process owner, the quality team, and the governing standard for your product.
Check the governing standard
Standards set the requirement for many processes. 3-A Sanitary Standards give guidelines for hygienic design for dairy and food equipment, and the ASME BPE Standards give guidelines on bioprocessing equipment, including its drainability, finish, and cleanability requirements. Holland’s guide to BPE and 3-A sanitary fittings explains how the two differ, and its post on who the ASME BPE is covers the committee behind the standard. A later post in this series covers 3-A and FDA certification.
Write the decision into the user requirements
Record the decision as a written requirement: CIP only, CIP with sanitize, or CIP with SIP, with the validated parameters. Component selection reads from that line. A decision that lives only in a meeting never reaches the purchase order.
Ready to solve this?
Share your product, cleaning chemistry, and sterility requirement, and Holland’s engineers will help you specify the right cleaning approach for your system.
How does the CIP or SIP decision change valve selection?
SIP raises the bar on every valve in the product path. The valve has to drain, tolerate steam temperature, and keep its seals intact through repeated thermal cycles. CIP asks for a cleanable valve with seals that tolerate the wash chemistry.
Valve types respond differently:
- Diaphragm valves: a weir-type body drains at its specified angle and the diaphragm isolates the product from the bonnet. Diaphragm valves are used most commonly in pharma/biotech because of their ability to drain and accept SIP applications.
- Ball valves: can accept higher temperatures and pressures so are many times used for SIP supply valves.
- Butterfly valves: the seat compound sets the temperature limit. Butterfly valves are not typically used in SIP applications.
- Check valves and other specialty valves: each one needs its seal compound confirmed for the hottest step.
A later post in this series compares butterfly, ball, and diaphragm valves in detail.
How does the CIP or SIP decision change gasket and elastomer selection?
Gaskets and elastomers fail first under the wrong chemistry or temperature, so the hottest and harshest step on the line sets the compound. A compound that survives CIP chemistry can fail under steam, and the reverse is also true.
Compound behavior in general terms:
- EPDM: certain EPDM compounds perform well with steam and with caustic and acid washes, but it swells in oils and fats.
- PTFE: resists nearly all chemistries and performs well with steam.
- Silicone: tolerates a wide temperature range, but repeated steam exposure shortens its life.
- FKM: certain FKM compounds perform well with steam. FKM also resists oils and fats.
Check the compound against every chemistry and temperature in the cycle. Holland’s overview of sanitary gasket elastomer materials and its chemical compatibility guide cover the options in more detail.
After thermal cycling, inspect gaskets and clamps for leaks and relaxation. Heat cycles can loosen a connection that sealed well at ambient temperature.
How does the CIP or SIP decision change pump and seal selection?
CIP and SIP place demands on the pump through its seals, its elastomers, and its drainability. The pump has to reach the CIP flow velocity, and on SIP lines the seal and elastomers have to tolerate steam temperature.
Three points apply to pump selection:
- Flow for CIP: the pump or a dedicated CIP supply pump has to deliver the velocity the cycle needs through all the lines served.
- Seal chemistry and temperature: the seal faces and elastomers see the wash chemistry and, on SIP lines, steam or hot condensate.
- Drainability: a pump casing and its piping have to drain, or liquid collects at the low point.
How does the CIP or SIP decision change instrumentation and piping design?
SIP changes instrumentation and piping the most. Sensors need steam-rated construction, piping needs slope and drains, and the layout needs a place for temperature monitoring at the coldest point. CIP asks for drainable piping, smooth finishes, and sensors that tolerate the wash chemistry.
Design points to carry onto the drawing:
- Slope and drainage: sloped, drainable piping is a core requirement in hygienic design. Confirm the slope requirement against the standard that governs your system.
- Dead legs: keep branches short, since a dead leg is a cold spot for SIP and a shadow for CIP. Holland’s post on good sanitary pump piping practice covers layout habits that help.
- Surface finish and welds: smooth product-contact surfaces and clean welds are easier to clean and sterilize. Holland’s guides to sanitary surface finish and to what makes a weld sanitary cover the specifications, and its comparison of passivation and electropolishing covers the finishing steps.
- Sensor ratings: temperature, pressure, and conductivity sensors need ratings for the hottest step they will see, plus compatibility with the wash chemistry.
- Steam traps and vents: specify them at every low point and at the sterile vent.
What are the most common CIP and SIP specification mistakes?
Five mistakes account for most of the gaps found at commissioning and audit. Each one traces back to a decision that was copied forward without checking the process.
- Over-specifying SIP on a CIP-only line. The line carries steam-rated components, traps, and sensors that never run a steam cycle.
- Under-specifying components on a SIP line. Gaskets, diaphragms, or instruments rated below steam temperature fail in service.
- Leaving dead legs in the design. Cold spots stay wet under SIP and stay soiled under CIP.
- Skipping coldest-point monitoring. The cycle appears to pass because the sensor sits at a warm location.
- Treating validation as a one-time event. A change in product, chemistry, or equipment needs a review of the cycle.
How do you specify the cleaning approach for a system in six steps?
Run these six steps for each system. The output is a written requirement, a component list that matches it, and a verification plan.
- Define the product risk. Write what a surviving organism would cost: spoilage, a recalled batch, or patient harm.
- Identify the governing standard. Name 3-A, ASME BPE, FDA requirements, or the customer standard that applies.
- Choose the approach. Write CIP only, CIP with sanitize, or CIP with SIP.
- Write the cycle parameters. List the steps, temperatures, concentrations, flow velocities, and hold times.
- Select components for the hottest and harshest step. Check valves, gaskets, seals, instruments, and piping against that step.
- Write the verification plan. List swab or rinse sampling, temperature records, and the review triggers.
Decide the cleaning approach before choosing components
CIP removes soil and runs first. SIP inactivates microorganisms and follows CIP on processes that need a sterile product path. Product risk and the governing standard decide which approach a system needs, and the answer reaches every valve, gasket, seal, instrument, and pipe in the product path.
Write the decision as a requirement before the first component is chosen. A line that only needs CIP then avoids the cost of steam-rated parts, and a line that needs SIP gets parts that can take it.
Ready to solve this?
Send over your process specs and Holland’s engineers will help you specify the right cleaning approach for your system.
Author
Holland Applied Technologies’ engineering team works daily with process and manufacturing engineers across pharma, biotech, and food and beverage manufacturing, specifying and supporting the sanitary and high-purity process equipment their lines depend on.
Related posts
- Reduce Cleaning Cycle Time by 80% by Using a Better Valve
- BPE and 3A Sanitary Fittings: What’s the Difference?
- An Overview of Sanitary Gasket Elastomer Materials
- What Is a Hydrophobic Sterile Tank Vent and Why Does It Need to Be Heated?
- What Is a Sanitary Surface Finish?